MIG-AC pulse power source for thin aluminium sheet
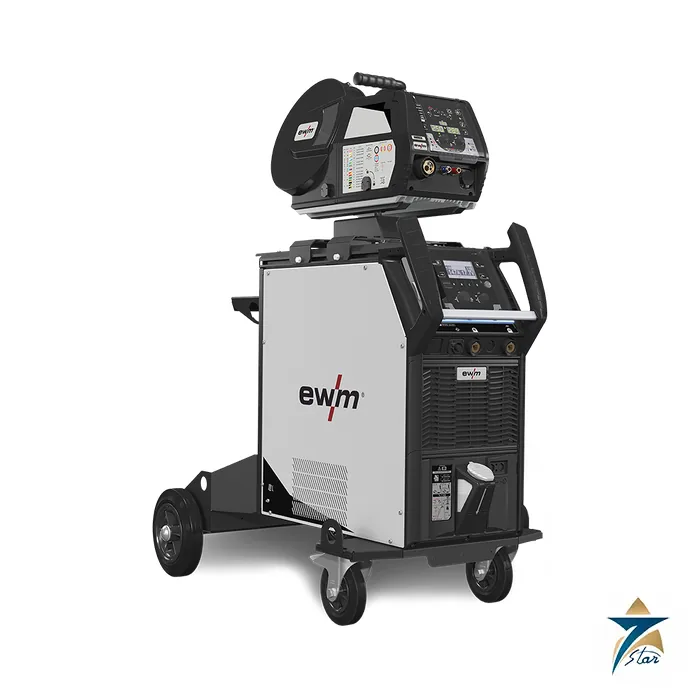
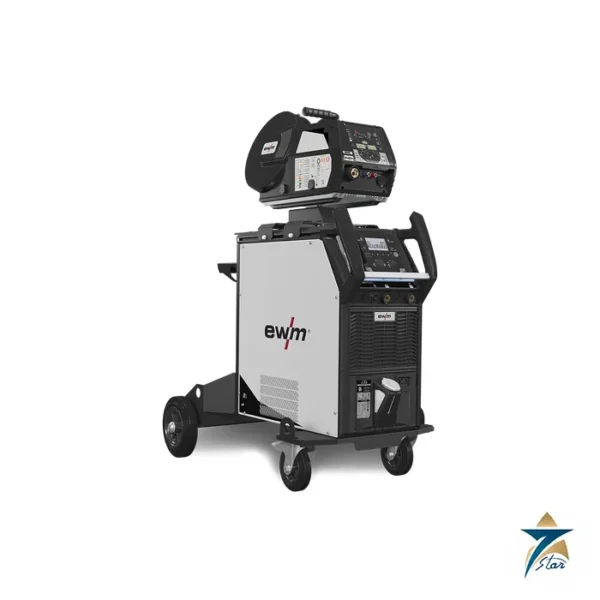
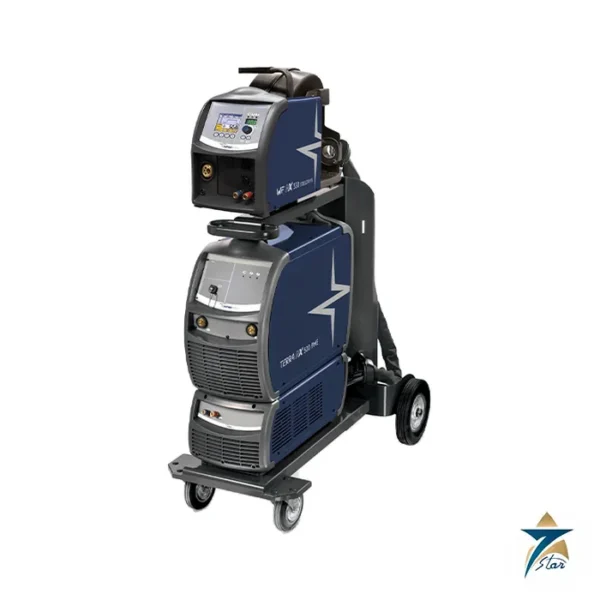
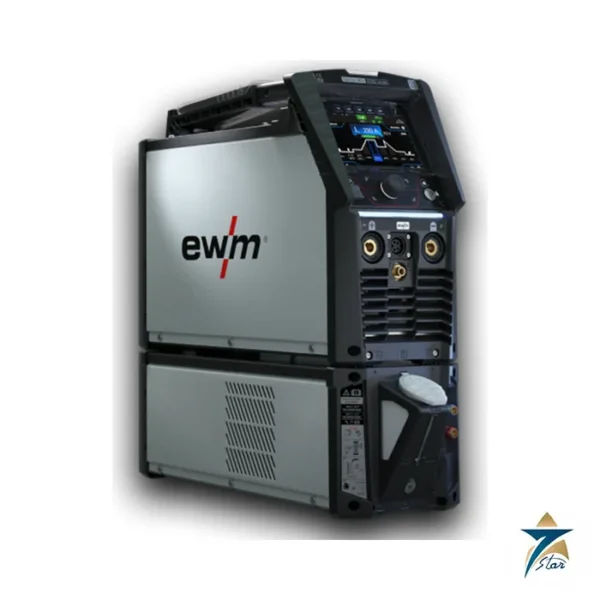
The EWM Titan XQ 400 AC puls is a 400 A water-cooled MIG/MAG power source that adds an alternating-current process, acArc puls XQ, to the standard DC processes of the Titan XQ range. In acArc puls XQ the polarity switches between a positive pulse phase and a negative phase: droplet formation and detachment take place in the positive phase, while in the negative phase heat moves from the workpiece into the wire. EWM describes the result as lower heat input, better gap bridging and less welding fume, which helps on thin aluminium sheet and AlMg alloys.
The machine pairs the Expert 2.0 XQ control with the Drive XQ wire feeder and EWM’s RCC (Rapid Current Control) inverter technology. All established DC processes are included at no extra cost, so one source covers aluminium AC work and steel or stainless MIG, TIG and MMA.
Technical specifications
| Parameter |
Specification |
| Manufacturer / model |
EWM / Titan XQ 400 AC puls |
| Processes |
MIG-AC puls (acArc puls XQ), MIG/MAG standard and pulse XQ, TIG, MMA, gouging |
| Welding current range |
5 A to 400 A |
| Duty cycle at 40 °C |
370 A at 100%; 400 A at 80% |
| Mains voltage, 50/60 Hz |
3 x 400 V (-25% to +20%) to 3 x 500 V (-25% to +10%) |
| Mains fuse (slow-blow) |
3 x 25 A |
| Maximum connected load |
18.6 kVA; recommended generator rating 25 kVA |
| Efficiency / power factor |
88% / cos phi 0.99 |
| Open circuit voltage at 400 V mains |
82 V |
| Cooling |
Fan-cooled machine; water-cooled torch, 8 l coolant tank |
| Control |
Expert 2.0 XQ with plain-text display |
| Protection class / EMC class |
IP 23 / A |
| Ambient temperature |
-25 °C to +40 °C |
| Standards |
IEC 60974-1, -2, -10 |
| Dimensions L x H x W (power source) |
1152 x 976 x 686 mm |
| Weight, water-cooled power source |
128 kg |
| Drive XQ wire feeder duty cycle |
470 A at 100%; 600 A at 40% (40 °C) |
| Drive XQ wire speed |
0.5 to 25 m/min, 4-roll drive (37 mm), Euro torch connector |
| Drive XQ spool / weight / size |
200 to 300 mm spool; 13 kg; 660 x 380 x 280 mm |
Processes included in the machine
Besides acArc puls XQ, the brochure lists rootArc and rootArc puls for root passes and gap bridging, coldArc and coldArc puls for thin sheet with minimal heat, forceArc and forceArc puls for a directionally stable, deep-penetration arc, wiredArc and wiredArc puls with penetration stabilisation under varying stick-out, Positionweld for positional welding, pulse XQ and standard XQ, and TIG, MMA and gouging.
EWM shows lap and fillet welds on 1.0 to 2.0 mm aluminium with 1.2 mm AlMg 4.5 wire in pure argon, at currents from 48 A to 73 A. Positionweld on top of acArc puls gives a regular, TIG-like seam appearance, and the arc is described as suitable for manual, automated and additive (3D) aluminium welding.
Configuration and installation notes
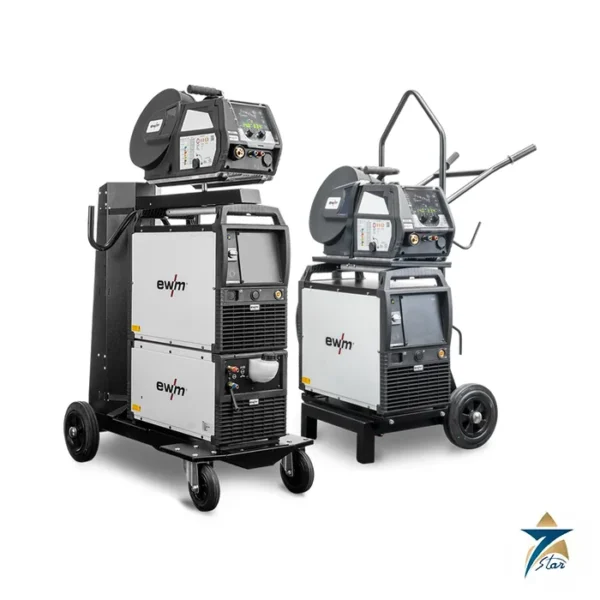
The Drive XQ feeder weighs 13 kg without spool and is designed for use on scaffolding or through manholes of 42 cm and above. Intermediate hose packages connect it to the power source, and the flexFit casing offers slot-nut mounting points for hose package holders and cross arms. An optional DGC electronic gas flow control opens the gas valve gently and meters gas for argon, mixed gas, CO2 or helium.
Plan for a 3-phase supply with 25 A slow-blow fuses and, for generator operation, a rating of at least 25 kVA. Aluminium wire needs suitable liners and torches; EWM offers a PM-RD3X function torch for aluminium work. Data logging and procedure management are available through the optional ewm Xnet 2.0 system.
Documents and quotation
The official EWM brochure (053-000079-00001), linked below, lists the process description and technical data for this machine. Other machines appear under MIG/MAG welding machines, including the Titan XQ 400 puls D.
For a quotation, state the mains supply, hose package length, torch type and any DGC or trolley options needed.
Why AC MIG helps on thin aluminium
In conventional DC pulsed MIG welding of aluminium, the wire is positive and most of the arc heat goes into the workpiece. On sheet of one or two millimetres this can cause burn-through, distortion and sagging, especially where fit-up gaps vary. The Titan XQ 400 AC puls alternates the polarity. During the negative phase more heat goes into melting the wire and less into the base metal, so the same deposition is achieved with lower heat input. The welder can therefore bridge wider gaps and weld thinner material with less risk of burn-through. The cleaning effect of the positive phase still breaks up the aluminium oxide layer, which is essential for sound fusion.
Lower heat input also reduces distortion, which saves straightening work on panels, enclosures, vehicle bodies and boat parts. EWM also notes reduced welding fume with acArc puls XQ, which improves conditions for the welder in enclosed workshops.
Selection guide for the Titan XQ 400 AC puls
- Choose this model when thin aluminium or AlMg alloys are a regular part of the work; for steel-only fabrication a DC Titan XQ puls machine is sufficient.
- Check the site supply: three-phase 400 V to 500 V with 25 A slow-blow fuses.
- Select the torch and liner for aluminium wire, and the intermediate hose package length for the distance between power source and feeder.
- Decide whether optional DGC gas flow control or Xnet 2.0 welding data management is needed.
- For automated or additive aluminium welding, confirm the robot or controller interface with the supplier.
Installation and maintenance
Install the power source on a level floor with free air flow to the fan, away from grinding dust. Fill the cooling unit with the coolant specified by EWM and check the level regularly; never run a water-cooled torch without coolant. For aluminium, keep the wire path short and clean, use the correct drive rolls, and store wire spools in a dry place to avoid oxide and porosity. Blow out the inside of the machine with dry compressed air at intervals suited to the dust level, and inspect cables, earth clamp and hose packages for damage. Periodic inspection and testing of welding equipment should follow IEC 60974-4 or local regulations.
Typical applications in Oman and the GCC
The Titan XQ 400 AC puls suits aluminium fabrication shops, marine and boat building, trailer and tanker bodies, architectural aluminium, HVAC and enclosures, and rail or transport components, as well as general steel and stainless work in the same workshop.
Why source from Seven Star LLC
Seven Star LLC supplies EWM welding machines and accessories across Oman and the GCC. Share your material, thickness and mains supply, and our team can help confirm the right configuration before you request a quote.

Reviews
There are no reviews yet.