- Automation & ControlView all 1,651 products
- AC Drives
- Industrial Communications
- PLC & I/O Cards
- Vibration Monitoring
- Automation Accessories
- Controllers & Data Acquisition
- CCTV & Security
- Safety Switches & Guard Locking
- Encoders
- Industrial Computers
- Servo Drives
- Motor Soft Starters
- HMI Displays
- Isolator & Barrier
- Pneumatic Cylinders
- Automation Software
- Machine Vision
- Robotics
















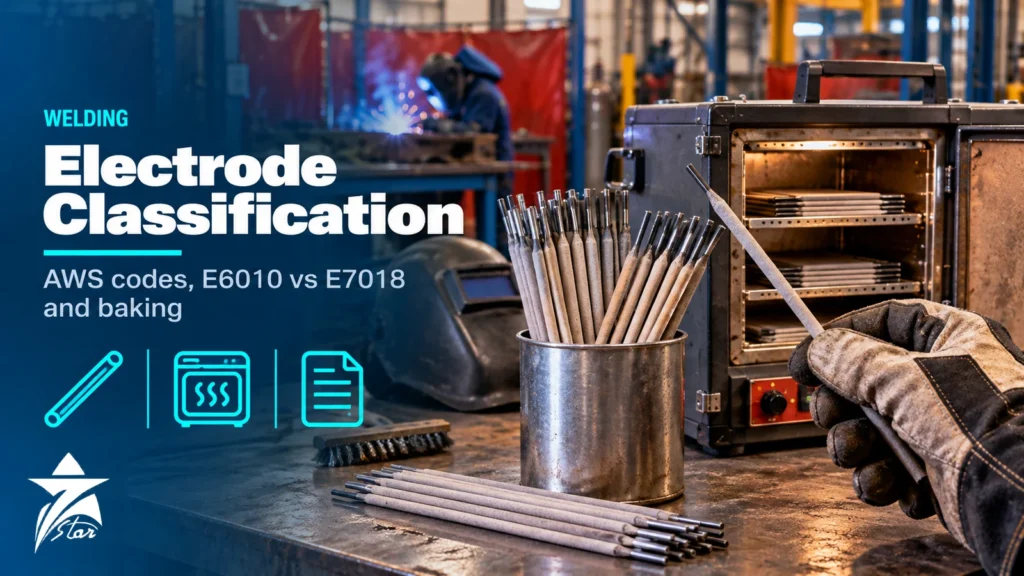
Welding electrode classification under AWS A5.1 and A5.5 packs strength, welding position, coating type, current and hydrogen level into a short code printed on every stick. Reading it correctly is the difference between a root pass that runs cleanly downhill on a pipeline and a cracked fillet weld on a thick, restrained structural joint. The most common confusion in the field, E6010 versus E7018, comes down to coating chemistry and hydrogen, and the most common failure in the Gulf is not the wrong electrode but the right electrode stored badly. This guide decodes A5.1 and A5.5 designations, compares the main coating types, explains when to use cellulosic and low-hydrogen electrodes, and sets out practical storage, holding and rebaking rules.
The Standards Behind Welding Electrode Classification
AWS A5.1/A5.1M covers carbon steel electrodes for shielded metal arc welding (SMAW), and AWS A5.5/A5.5M covers low-alloy steel electrodes, meaning steels where no single alloying element exceeds 10.5%. Stainless steel electrodes are covered separately by AWS A5.4. Internationally, ISO 2560 classifies covered electrodes for non-alloy and fine-grain steels, and many electrode packages show both the AWS and ISO designations. The A5.1M metric system expresses strength in MPa, so E6010 becomes E4310 and E7018 becomes E4918; the coating and position digits stay the same.
Decoding an A5.1 Designation
Take E7018-1 H4R as an example and read it left to right:
- E: covered electrode for arc welding.
- 70: minimum tensile strength of the weld metal in ksi (70 ksi, about 490 MPa). An E60XX electrode is 60 ksi (about 430 MPa).
- 1 (third digit): welding position. 1 = all positions; 2 = flat and horizontal fillet only; 4 = flat, horizontal, overhead and vertical-down, as in E7048.
- 8 (last digit, read with the third): coating type and usable current. Here, low-hydrogen potassium with iron powder, AC or DC electrode positive.
- -1: optional designator for improved impact toughness at lower temperature than the base classification.
- H4: optional diffusible hydrogen designator: average not more than 4 ml per 100 g of deposited weld metal. H8 and H16 indicate 8 and 16 ml/100 g.
- R: optional designator showing the electrode passed the specification’s absorbed-moisture test after humid exposure.
Common A5.1 Electrodes Compared
| Classification | Coating | Current | Positions | Typical use |
|---|---|---|---|---|
| E6010 | High-cellulose sodium | DCEP | All | Pipeline and pipe root passes, deep penetration, dirty or rusty steel |
| E6011 | High-cellulose potassium | AC or DCEP | All | Similar to E6010 where only AC transformer sets are available |
| E6013 | High-titania potassium (rutile) | AC, DCEP or DCEN | All | Light fabrication, sheet metal, general maintenance; easy arc, smooth bead |
| E7016 | Low-hydrogen potassium | AC or DCEP | All | Low-hydrogen work, often favoured for root runs where E7018 iron powder is less suited |
| E7018 | Low-hydrogen potassium, iron powder | AC or DCEP | All | Structural, pressure vessel and piping fill and cap passes; crack-sensitive steels |
| E7024 | Iron powder, titania | AC, DCEP or DCEN | Flat and horizontal fillet | High-deposition fillets in the flat position |
| E7048 | Low-hydrogen potassium, iron powder | AC or DCEP | Including vertical-down | Low-hydrogen vertical-down welding on thin sections and structures |
E6010 vs E7018: Choosing Between Cellulosic and Low-Hydrogen
The two most specified electrodes in oil and gas work are opposites by design.
E6010 and Other Cellulosic Electrodes
The cellulose in the coating burns to produce a forceful, gas-shielded arc with deep penetration and a thin, fast-freezing slag. That makes cellulosic pipeline electrodes the traditional choice for vertical-down root and hot passes in cross-country pipelines welded to API 1104, for open-root joints and for steel with some surface contamination. The price is hydrogen: cellulose combustion produces hydrogen-rich gas and the weld metal carries high diffusible hydrogen. On higher-strength steel, heavy walls or high-restraint joints this raises the risk of hydrogen-induced cold cracking, controlled in pipeline practice with preheat, fast hot-pass timing and qualified procedures. Higher-strength cellulosic grades for pipeline steels, such as E8010-P1, are classified under A5.5.
E7018 and Other Low-Hydrogen Electrodes
The basic (lime-fluoride) coating of E7018 contains almost no hydrogen-bearing compounds, giving low diffusible hydrogen, good impact toughness and smooth, X-ray quality welds when used with correct technique. E7018 is the default for structural steel to AWS D1.1, for pressure equipment and process piping fill and cap passes, and for any steel with a high carbon equivalent or thick section. It requires a short arc, careful starts to avoid start porosity and, above all, dry electrodes: its low-hydrogen status lasts only as long as the coating stays dry.
- Choose E6010 for open-root pipe roots, vertical-down pipeline spreads and contaminated surfaces, within a qualified procedure that manages hydrogen.
- Choose E7018 for fill and cap on pipe, for structural and pressure welds, for thick or restrained joints and where impact toughness is specified.
- A common combination on process piping is a GTAW or E6010 root followed by E7018 fill and cap, provided the WPS qualifies it.
Reading A5.5 Low-Alloy Designations
A5.5 electrodes use the same strength, position and coating digits, followed by a suffix for weld-metal chemistry. The most common suffixes in plant work are:
- A1: carbon–molybdenum (about 0.5% Mo), for C-½Mo piping and vessels.
- B2, B3 (and related B-series): chromium–molybdenum, for example B2 for 1¼Cr-½Mo and B3 for 2¼Cr-1Mo creep-resistant steels in boilers, heaters and hot hydrogen service.
- C1, C2, C3: nickel steels for low-temperature toughness.
- D-series: manganese–molybdenum for higher strength.
- P1: pipeline electrodes, including cellulosic E7010-P1 and E8010-P1.
- W: weathering steel electrodes.
- G: general classification where composition is agreed between supplier and purchaser; always check the actual chemistry on the certificate.
Examples include E8018-B2 for 1¼Cr-½Mo piping, E9018-B3 for 2¼Cr-1Mo and E8018-C3 for low-temperature service. Low-alloy electrodes for creep-resistant steels normally require preheat and post-weld heat treatment set out in the WPS.
Storage, Holding Ovens and Rebaking
Low-hydrogen electrodes pick up moisture from the air through their coating, and the absorbed water becomes diffusible hydrogen in the weld. Storage rules exist for that single reason. Always follow the manufacturer’s data sheet and the governing code, but typical practice is:
- Keep unopened low-hydrogen electrodes in their sealed (hermetic or vacuum) packaging in a dry store. Vacuum-packed electrodes can usually be used directly from a freshly opened pack within the exposure time printed on it.
- Once a conventional can is opened, transfer the electrodes to a heated holding oven. AWS D1.1 sets a minimum holding temperature of 120 °C (250 °F) for low-hydrogen electrodes.
- Issue electrodes to welders in heated portable quivers and limit atmospheric exposure. Structural codes set maximum exposure times, commonly 4 hours for standard E70XX and longer for electrodes with the R moisture-resistant designator; humid conditions justify shorter limits.
- Rebake electrodes that exceed exposure limits at the manufacturer’s stated temperature and time, commonly in the range of 260–430 °C (500–800 °F) for one to two hours, then return them to the holding oven. Many codes and procedures allow only one rebake.
- Discard electrodes that were wet, have damaged or cracked coatings, or whose rebaking history is unknown.
Cellulosic electrodes are the exception: they rely on a certain moisture content in the coating for their arc characteristics. They should be kept dry in their original packaging at normal ambient conditions and must never be put through a low-hydrogen rebake cycle, which dries out the coating and spoils arc performance. Rutile electrodes such as E6013 are stored dry and may be dried at moderate temperature if damp, according to the maker’s instructions. Suitable electrode drying ovens and quivers, with calibrated thermostats and temperature records, should be part of every fabrication site’s quality system.
Gulf Conditions: Humidity, Heat and Sour Service
Coastal sites in Oman and across the GCC combine high temperature with high humidity, especially on summer nights and mornings, which accelerates moisture pickup in exposed low-hydrogen electrodes. Practical responses include using vacuum-packed or R-designated electrodes, shortening exposure times in the site procedure, keeping holding ovens running on reliable power and logging oven temperatures. Dust ingress into open cans and quivers is another issue; keep lids closed. For sour (H2S) service, NACE MR0175/ISO 15156 limits weld hardness and restricts nickel in carbon steel weld metal, so electrode selection, procedure qualification and hardness testing must be checked against the project specification.
Common Mistakes With Covered Electrodes
- Leaving opened E7018 cans in the workshop overnight and using them the next day without rebaking.
- Rebaking cellulosic E6010 electrodes in the same oven cycle as E7018.
- Mixing similar-looking electrodes; always check the imprint on the coating near the grip end.
- Using E7018 on AC with a power source that has low open-circuit voltage, causing hard starts; check the electrode’s AC suitability and the machine’s OCV.
- Treating a G suffix as equivalent to a specific alloy classification without checking chemistry.
- Selecting electrodes by tensile strength only and ignoring impact toughness requirements at minimum design metal temperature.
Welding Electrode Classification and Selection Checklist
- Base metal specification, grade, thickness and carbon equivalent.
- Governing code and WPS: AWS D1.1, ASME Section IX with B31.3 or B31.1, API 1104 or project specification.
- Required tensile strength and impact toughness at the specified test temperature.
- Welding positions, joint type and whether vertical-down is required.
- Available current type (AC or DC) and power source characteristics from your stick welding machines.
- Hydrogen limit (H4, H8) and moisture resistance (R) requirements.
- Sour service, PWHT or elevated temperature requirements.
- Storage, holding and rebake facilities on site.
Welding Electrodes We Supply
These examples follow the AWS classifications explained above.
| Product | Type | Where it fits |
|---|---|---|
| LongTeng E6013 Carbon Steel Welding Electrode | E6013 rutile electrode | General fabrication in all positions. |
| LongTeng E7018 Low Hydrogen Carbon Steel Welding Electrode | E7018 low hydrogen electrode | Structural and pressure work where hydrogen cracking is a risk. |
| LongTeng E7015 DC Low Hydrogen Carbon Steel Welding Electrode | E7015 low hydrogen electrode | DC welding of carbon steel. |
| LongTeng E308-16 Stainless Steel Welding Electrode | E308-16 stainless electrode | Welding 304 stainless steel. |
| LongTeng E309-16 Stainless Steel Welding Electrode | E309-16 stainless electrode | Joining stainless steel to carbon steel. |
| Hyundai SR-625 ENiCrMo-3 Nickel Alloy 625 Welding Electrode | ENiCrMo-3 nickel alloy electrode | Alloy 625 and dissimilar metal joints. |
Send the AWS class, diameter and quantity, or the WPS requirement, through our quote request form.
Sourcing Welding Electrodes Through Seven Star LLC
Seven Star LLC supplies carbon steel, low-alloy and cellulosic welding electrodes, along with other welding consumables, electrode drying and holding ovens and portable quivers on request for fabrication and maintenance work in Oman and the GCC. We can help cross-check AWS and ISO classifications, alternative manufacturers’ equivalents and certificate requirements. Availability and lead time are confirmed at quotation.
Need electrodes for a specific WPS or project? Send us the AWS classification, diameter, quantity, required certificates and any hydrogen or sour-service limits, and we will return a quotation with matching options.
Frequently asked questions
What do the numbers in E7018 mean?
E means covered electrode, 70 means 70 ksi (about 490 MPa) minimum weld metal tensile strength, 1 means all positions, and the final 8 (read with the 1) indicates a low-hydrogen potassium coating with iron powder usable on AC or DCEP. Optional suffixes such as -1, H4 and R add toughness, hydrogen and moisture-resistance information.
What is the difference between E6010 and E7018?
E6010 has a cellulosic coating that gives a forceful, deeply penetrating arc ideal for open-root and vertical-down pipe welding, but with high diffusible hydrogen. E7018 has a low-hydrogen basic coating that gives tougher, crack-resistant welds for structural and pressure work, but it must be kept dry in holding ovens.
At what temperature should E7018 electrodes be stored?
After the sealed can is opened, low-hydrogen electrodes are kept in a holding oven; AWS D1.1 sets a minimum of 120 °C (250 °F). Rebaking, when exposure limits are exceeded, is done at the manufacturer's stated temperature, commonly in the 260–430 °C range.
Can E6010 electrodes be baked like E7018?
No. Cellulosic electrodes need a certain moisture content in the coating to produce their arc characteristics, and high-temperature baking dries them out and spoils performance. Store them dry in their original packaging at ambient conditions.
What does the H4 designator mean on an electrode?
H4 means the average diffusible hydrogen in the weld metal is not more than 4 ml per 100 g of deposited metal, measured under the specification's test conditions. H8 and H16 indicate 8 and 16 ml per 100 g.
What does E8018-B2 mean in AWS A5.5?
It is an 80 ksi minimum tensile, all-position, low-hydrogen iron-powder electrode whose B2 suffix indicates 1¼Cr-½Mo weld metal. It is used for welding matching chromium–molybdenum piping and vessels, normally with preheat and post-weld heat treatment.
Was this guide helpful?One click helps us write better guides for engineers.
Thank you! Glad it helped. Need this equipment for your project? Request a quotation
Thank you. We will use this to improve the guide.