Low-carbon, higher-silicon MIG wire for 304 stainless
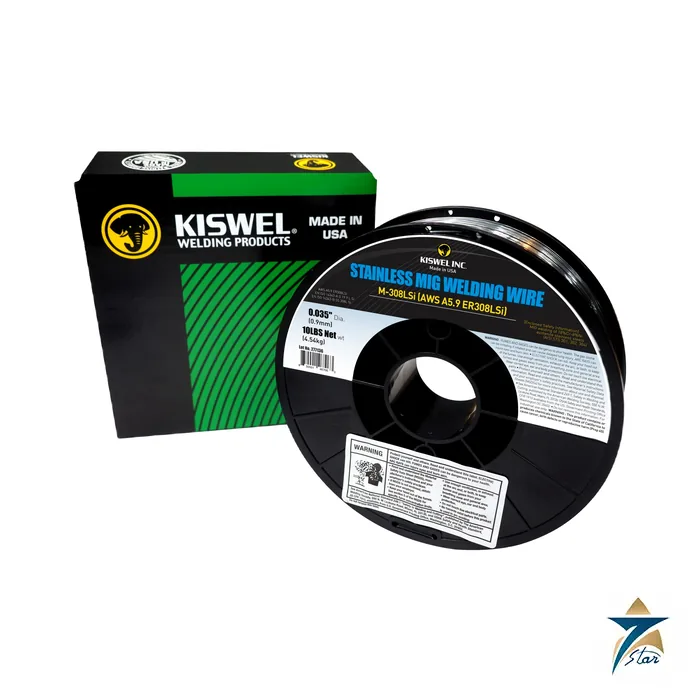
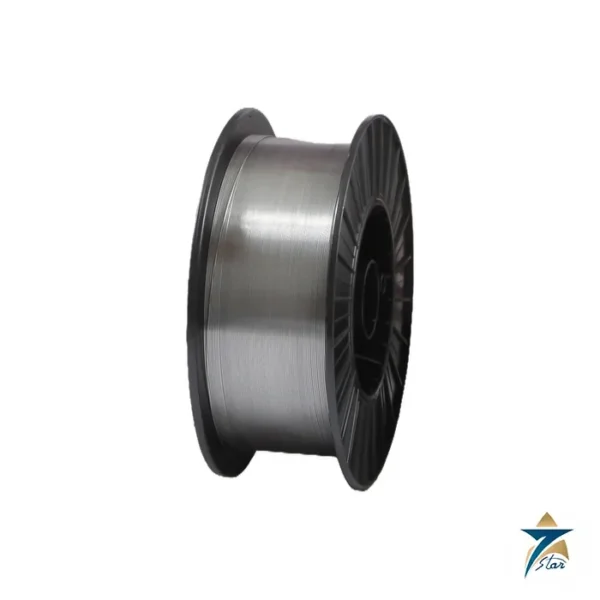
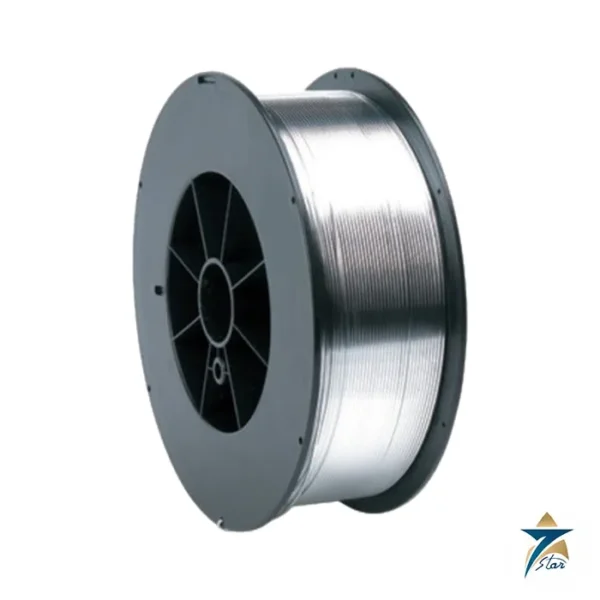
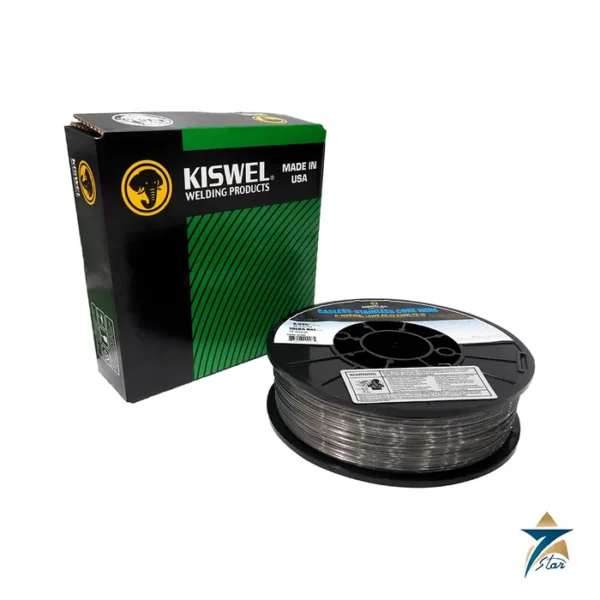
The KISWEL M-308LSi is a solid stainless steel wire for MIG welding of low-carbon 18% Cr, 8% Ni austenitic steels such as AISI 301, 302 and 304. KISWEL lists petrochemical equipment and nuclear power plant apparatus among its applications.
It is the silicon-enhanced version of the 308L grade. The higher silicon level improves wetting and bead flow in MIG welding, which helps produce flatter fillets and smoother toe transitions than a standard-silicon 308L wire.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
KISWEL / M-308LSi |
| Process |
GMAW (MIG), solid stainless wire |
| AWS A5.9-2012 |
ER308LSi |
| EN ISO 14343-A / -B:2009 |
G 19 9 L Si / SS 308L Si |
| JIS Z 3321:2013 |
YS308LSi |
| Typical wire chemistry, % |
C 0.01, Si 0.85, Mn 1.68, Ni 9.89, Cr 19.63 |
| Typical all-weld metal |
YS 399 MPa, TS 619 MPa, El. 43% |
| Typical impact energy |
114 J at 0 °C; 60 J at -196 °C |
| AWS A5.9 requirement |
TS ≥520 MPa, El. ≥35% |
| EN ISO 14343 requirement |
YS ≥320 MPa, TS ≥510 MPa, El. ≥30% |
| Kiswel Inc. pack (USA) |
0.035 in (0.9 mm), 10 lb spool |
Selecting 308LSi against 308L and 316LSi
The very low carbon content of 0.01% in the typical wire analysis limits chromium carbide precipitation in the heat-affected zone and weld, which protects against intergranular corrosion in 304L and similar grades. The typical impact value of 60 J at -196 °C shows that the deposit keeps useful toughness at cryogenic temperatures, although any low-temperature service needs its own procedure qualification.
Choose 308LSi over plain 308L when bead appearance and wetting in short-arc, spray or pulsed MIG are the priority. Where the base metal contains molybdenum, such as 316L, a 316LSi wire is the matching choice; for joints between stainless and carbon steel a 309L-type over-alloyed filler is usually specified. These are general selection rules, not KISWEL statements.
Shielding gases for austenitic stainless MIG welding are normally argon with a small addition of oxygen or CO2. Confirm the gas and transfer mode in your procedure. For carbon steel MIG work, see the KISWEL KC-28 ER70S-6 wire.
Cleanliness has a strong effect on stainless weld quality. Use dedicated stainless steel brushes and grinding discs, degrease the joint area, and protect spools from shop dust. Heat tint left after welding lowers corrosion resistance, so pickle or mechanically clean the weld zone when the service environment is aggressive.
The values in the table are typical test results from the KISWEL catalogue, not guaranteed figures. The procedure qualification record should refer to the classification minimums. Wire diameter and spool format should match the feeder rolls, liners and contact tips used in the cell.
Where a code requires ferrite measurement, the ferrite number of the deposit depends on dilution, heat input and shielding gas, so it should be checked on the procedure test piece rather than estimated from the wire analysis alone.
Documents and quotation
The KISWEL M-308LSi catalogue datasheet is attached. Other MIG wires are in our Solid Welding Wire category.
For a quotation, state the diameter, spool type and weight, quantity, and whether an EN 10204 3.1 certificate is required.
M-308LSi Classifications & Typical Properties
- AWS A5.9 ER308LSi; EN ISO 14343 G 19 9 L Si; JIS YS308LSi.
- Shielding gas Ar + 2% O2; polarity DC electrode positive.
- Typical wire chemistry: 0.01% C, 0.85% Si, 19.63% Cr, 9.89% Ni.
- Typical weld metal: yield strength 380 MPa, tensile strength 580 MPa, elongation 40%, impact 180 J at 0 °C and 80 J at −196 °C.
Selection & Ordering Guide for the M-308LSi
The M-308LSi is offered in 0.8 to 1.6 mm diameters. KISWEL lists about 70–250 A for 0.9 mm, 100–300 A for 1.2 mm and 120–320 A for 1.4 mm wire. Use it for 304 and 304L type stainless steels; for molybdenum-bearing 316L choose a 316LSi wire.
How the M-308LSi Works
The extra silicon in the LSi grade improves wetting and fluidity of the weld pool, giving flatter beads and smoother toes than standard 308L, which helps in MIG/MAG welding of stainless sheet and pipe. The low carbon content reduces the risk of carbide precipitation and intergranular corrosion, and the good low-temperature toughness supports cryogenic duty.
Typical Applications in Oman & the GCC
KISWEL lists nuclear, petrochemical and plant applications. In Oman and the GCC the M-308LSi is used for stainless piping, tanks, food and water treatment equipment and general stainless fabrication.
Storage & Handling
Keep consumables in their original sealed packaging in a dry, ventilated store, away from direct contact with floors and walls, and use the oldest stock first. In the humid coastal climate of Oman and the GCC, open only as much product as will be used in a shift and protect partly used spools or cans from moisture and dust. Follow the handling and re-drying instructions given by KISWEL for the specific product.
Why Source from Seven Star LLC
Seven Star LLC supplies KISWEL welding consumables across Oman and the GCC. Send the classification, diameter, quantity and any approval or certificate requirements, and request a quote; our team can help confirm the correct ordering code and packaging.
Welding Practice Tips for the M-308LSi
Consistent results come from good preparation and stable settings. Clean the joint of mill scale, rust, oil, paint and moisture before welding, and fit up the joint with a uniform gap. Set the current and voltage within the manufacturer range for the chosen diameter and position, then fine-tune on a test piece before production. Keep a steady travel speed and the recommended electrical stick-out, because changes in stick-out alter the current and therefore the bead shape and penetration. Check the wire feed path, contact tip size and feed rolls so the wire feeds smoothly without kinking. Where a welding procedure specification applies, follow the qualified parameters, interpass temperature limits and inspection requirements, and record the batch or lot number of the consumable used for traceability.

Reviews
There are no reviews yet.