- Automation & ControlView all 1,744 products
- AC Drives
- Industrial Communications
- PLC & I/O Cards
- Vibration Monitoring
- Automation Accessories
- Controllers & Data Acquisition
- CCTV & Security
- Safety Switches & Guard Locking
- Isolator & Barrier
- Encoders
- Industrial Computers
- Servo Drives
- Motor Soft Starters
- HMI Displays
- Pneumatic Cylinders
- Automation Software
- Machine Vision
- Robotics
















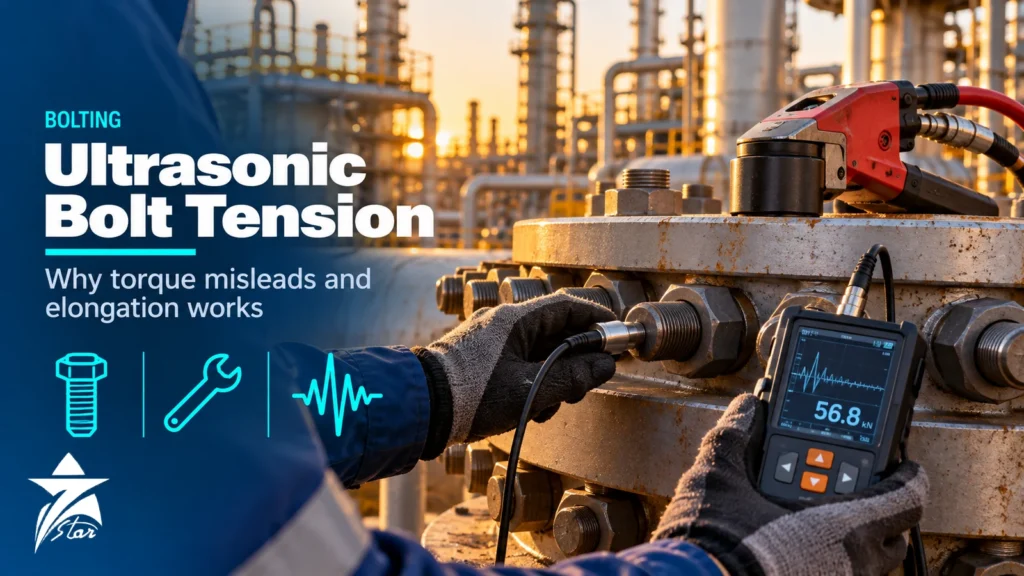
Ultrasonic bolt tension measurement answers the question a torque wrench cannot: how much clamp load is actually in this bolt? On a leaking flange, a loose turbine casing or a cracked coupling bolt, the real cause is usually the wrong preload, and the torque record says nothing useful about it because most of the applied torque is spent on friction. This guide explains why torque is an unreliable proxy for preload, how ultrasonic elongation measurement works, how to calibrate it for your bolts, where it pays off in oil and gas, power and petrochemical plants, and the practical mistakes that ruin readings in the field.
Why Torque Is a Poor Measure of Preload
What a joint needs is clamp force. Torque is only an indirect way to get there, and the conversion depends on friction at two surfaces: the threads and the nut or bolt-head bearing face. Fastener literature commonly illustrates the split as roughly 50% of input torque lost under the nut or head, about 40% in the threads, and only around 10% converted into bolt tension. Those proportions change with every variable that affects friction:
- Lubricant type, quantity and whether it was applied to the threads only or to the bearing face as well.
- Surface coatings such as zinc, zinc-nickel or fluoropolymer, and their condition after previous use.
- Thread condition: rust, galling, damage and burrs on reused studs and nuts.
- Washer hardness and flatness, and the surface finish of the flange spot face.
- Tightening speed and the tool used.
Friction coefficients commonly vary by around ±20% even with nominally identical parts, and because the bolt only receives a small fraction of the torque, that variation translates into large preload scatter between bolts that were all tightened to the same torque. The usual short formula, T = K × F × d (torque equals nut factor times preload times nominal diameter), shows the problem directly: the nut factor K is an empirical value that lumps all friction effects together, and it is seldom known accurately for the actual bolt on the actual day.
Bolt Load Control Methods Compared
| Method | What is controlled | Typical accuracy of preload | Comments |
|---|---|---|---|
| Torque wrench | Applied torque | Lowest; depends on friction | Fast and cheap, acceptable for non-critical joints |
| Torque-angle (turn of nut) | Rotation after snug | Better than torque alone | Sensitive to snug point and joint stiffness |
| Hydraulic tensioning | Applied axial load before nut run-down | Good on load applied; loses some on transfer to nut | Needs extra thread length and access space |
| Direct tension indicators | Washer deformation | Indicates minimum load reached | Mainly structural bolting; one-time use |
| Strain-gauged bolts | Bolt strain | High | Special bolts, wiring, cost |
| Ultrasonic elongation | Change in acoustic length of the bolt | High when calibrated on the bolt lot | Works on standard bolts with prepared ends; can be repeated in service |
How Ultrasonic Bolt Elongation Measurement Works
When a bolt is tightened, it stretches elastically in proportion to the load within its stressed length. An ultrasonic bolt gauge sends a longitudinal wave from a transducer on one end of the bolt, measures the time of flight to the opposite end and back, and compares it with the time measured before tightening. The change in time comes from two effects that act in the same direction:
- Physical elongation: the bolt is longer, so the sound travels further.
- Acoustoelastic effect: tensile stress slightly reduces the sound velocity in steel, so the sound also travels more slowly.
The instrument combines both effects through a material stress factor and converts the time change into elongation and then into load or stress, using the bolt’s effective length, cross-section and modulus. Because the measurement is of the bolt itself, friction does not enter into it.
Single-Wave and Dual-Wave Methods
The common single-wave (longitudinal) method needs a zero-load reference reading for each bolt, taken before installation, so every bolt must be identified and its reference stored. Dual-wave methods measure both longitudinal and transverse (shear) wave times; because the two wave types respond differently to stress, their ratio indicates load without an unloaded reference, which is useful for bolts already installed. Dual-wave measurements usually need bolt-specific calibration and higher signal quality, so check the instrument’s capability before relying on it.
Effective Length, Temperature and Calibration
Three inputs decide the accuracy of an ultrasonic bolt reading.
Effective Length
Stress is not uniform along a bolt. The full stress exists in the grip between the nut and head, but part of the threads inside the nut and part of the head also stretch. Instrument makers define an effective length as the grip length plus an allowance for these regions. Entering the wrong grip length directly scales the load error, so measure grip on the actual joint, including gaskets and washers.
Temperature
Steel expands with temperature and sound velocity falls with temperature, so a bolt that warms up between reference and final readings appears to have stretched. Gauges compensate using a temperature coefficient and a measured bolt temperature, either entered manually or read by a temperature probe. Always measure the bolt temperature at the time of each reading, not the air temperature.
Load Factor Calibration
Handbook material constants give reasonable results, but the best accuracy comes from calibrating a sample of the actual bolt lot in a load cell or tensile machine, recording time of flight against known load and deriving a load factor. Published laboratory work reports errors of a few percent once effective length is corrected, a large improvement over torque-based methods. Calibration is especially important for short bolts, where the total elongation is small and small timing errors are proportionally larger.
Preparing Bolts for Ultrasonic Measurement
- Face or grind the bolt ends flat and parallel; the transducer end must give a clean, stable echo from the opposite end.
- Remove paint, scale and marking from the measurement face, or specify bolts supplied with prepared ends.
- Mark each bolt with a unique identifier that matches the gauge’s memory location.
- Take and store the zero-load reference reading and temperature before installation.
- Use the transducer size and frequency recommended for the bolt diameter; magnetic holders keep alignment steady on vertical studs.
- Apply a thin, consistent layer of couplant; air gaps and thick layers both change the timing.
Where Ultrasonic Bolt Measurement Pays Off
- Critical flanged joints on high-pressure, high-temperature and toxic or sour service, where leaks are expensive and dangerous; ASME PCC-1 lists ultrasonic measurement among bolt load control methods.
- Turbine and compressor casings, split lines and coupling bolts, where uneven preload causes distortion and fatigue.
- Reciprocating compressor and engine connecting rod and main bearing bolts.
- Wind turbine, structural and foundation anchor bolts, where periodic checks detect relaxation without loosening.
- Heat exchanger channel covers and large-diameter girth flanges that leak after thermal cycling.
- Verification of hydraulic tensioning, to measure the real residual load after transfer to the nut.
Instrument Options
Portable handheld bolt tension instruments are used for installation and maintenance checks on site. Bench-top bolt tension instruments suit laboratories and assembly lines where many identical bolts are measured and data must be logged. Where joints must be monitored over time, remote monitoring systems with permanently bonded transducers record bolt load without disturbing the joint. All three instrument types are grouped in the bolt tension category, and earlier background on one manufacturer’s monitors is available in our guide to Dakota NDT tension monitors.
Ultrasonic Bolt Tension Measurement: Common Mistakes and Troubleshooting
- No reference reading: a single-wave measurement on an already tightened bolt without a zero-load reference cannot give absolute load.
- Wrong grip length: the most frequent cause of systematic error; measure it on the assembled joint.
- Temperature taken from air: bolts in sun or on hot flanges can be far from ambient; use a contact probe.
- Poor end preparation: rounded, stamped or rusty ends give weak or unstable echoes.
- Wrong echo: on bolts with central holes, reduced shanks or threads near the end, the gauge can lock on a mode-converted or geometric echo; check the waveform.
- Over-reliance on handbook constants for high-alloy or non-standard bolt materials instead of a load-factor calibration.
GCC Field Conditions
Hot climates complicate bolt measurement more than most NDT tasks. A stud on a sun-exposed flange in an Omani summer can be tens of degrees warmer than the same stud measured at dawn, so reference and final readings must both be temperature-compensated with measured bolt temperature. Sour service bolting (for example B7M studs and 2HM nuts, with restricted hardness) and coated studs used against corrosion in coastal plants change thread friction, which is one more reason torque-only tightening gives inconsistent load. Dust and humidity make clean end faces and fresh couplant essential, and work in hazardous areas requires the gauge and accessories to be accepted under the site permit system.
Ultrasonic Bolt Tension Measurement Checklist
- Joint drawing with bolt material, grade, diameter, length and target preload.
- Bolt ends prepared flat and parallel, each bolt uniquely marked.
- Grip length measured on the assembled joint and effective length entered.
- Load factor from calibration on the bolt lot, or documented material constant.
- Zero-load reference reading and bolt temperature recorded for each bolt.
- Tightening pattern and passes defined; final readings recorded with temperature.
- Follow-up checks scheduled for relaxation after thermal cycling or gasket creep.
Bolt Tension Monitors We Supply
These Dakota instruments measure bolt elongation ultrasonically, the method explained in this guide.
| Product | Type | Where it fits |
|---|---|---|
| Dakota BT1-DL Bolt Tension Monitor | Portable bolt tension monitor | Field measurement on flanges, structures and machinery. |
| Dakota BT2-DL Benchtop Bolt Tension Monitor | Benchtop bolt tension monitor | Laboratory and workshop measurement. |
| Dakota MultiMax – 4 Channel Bolt Tension Monitor | 4-channel bolt tension monitor | Monitoring several bolts at once during tightening. |
Send the bolt size, length and material through our quote request form, and we will match the instrument and transducers.
Sourcing Bolt Tension Instruments Through Seven Star LLC
Seven Star LLC supplies handheld and bench-top ultrasonic bolt tension instruments, bolt transducers, temperature probes, couplants and remote monitoring systems on request for plants and contractors in Oman and the GCC. We can help with selection and with cross-checking transducer and accessory part numbers against your existing gauges. Availability and lead time are confirmed at quotation.
Planning ultrasonic bolt load control on a critical flange or machine? Send us the bolt specification, joint details or your current instrument model, and we will quote a suitable gauge, transducers and accessories.
Frequently asked questions
Why is torque not an accurate way to set bolt preload?
Most of the applied torque is used to overcome friction under the nut and in the threads, and only a small fraction, often illustrated as about 10%, becomes bolt tension. Small changes in lubrication, coating or thread condition therefore cause large differences in preload between bolts tightened to the same torque.
How does an ultrasonic bolt gauge measure tension?
It measures the time of flight of an ultrasonic pulse along the bolt before and after tightening. The change comes from the physical stretch of the bolt and the reduction of sound velocity under stress, and the instrument converts it into elongation and load using the effective length and a material or calibrated load factor.
Do I need a reference reading before tightening?
With the common single-wave longitudinal method, yes: each bolt needs a zero-load reference reading stored before installation. Dual-wave methods that combine longitudinal and shear waves can estimate load without a prior reference, but they usually need bolt-specific calibration.
How accurate is ultrasonic bolt tension measurement?
When the load factor is calibrated on the actual bolt lot and effective length and temperature are handled correctly, errors of a few percent are reported. Accuracy is lower with handbook constants, short bolts with small elongation, or poorly prepared bolt ends.
How should bolts be prepared for ultrasonic measurement?
Both ends should be flat and parallel, free of paint, scale and stamped markings at the transducer face, and each bolt should carry a unique identifier. Some users specify studs with factory-prepared ends for critical joints.
Does temperature affect ultrasonic bolt readings?
Yes. Thermal expansion and the drop in sound velocity with temperature both lengthen the measured time of flight, so a warmer bolt appears to carry more load. Gauges compensate using the measured bolt temperature, which should be taken at each reading.
Was this guide helpful?One click helps us write better guides for engineers.
Thank you! Glad it helped. Need this equipment for your project? Request a quotation
Thank you. We will use this to improve the guide.