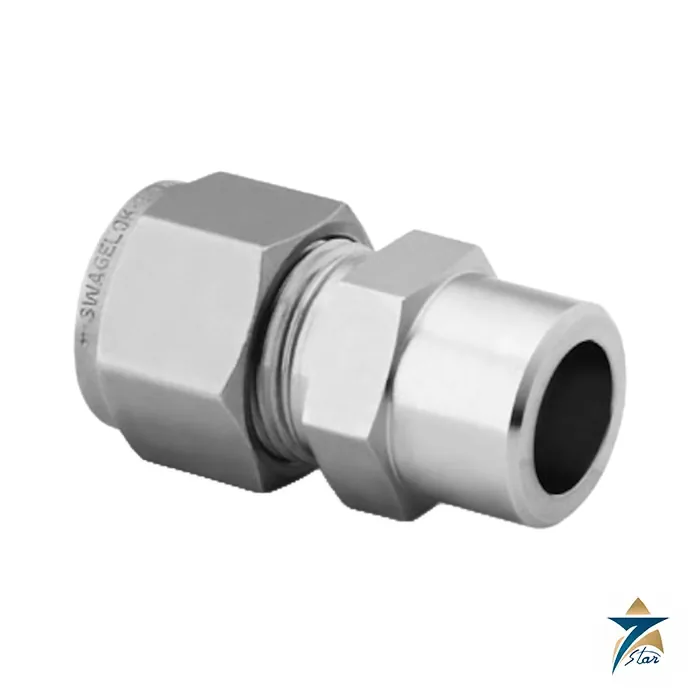
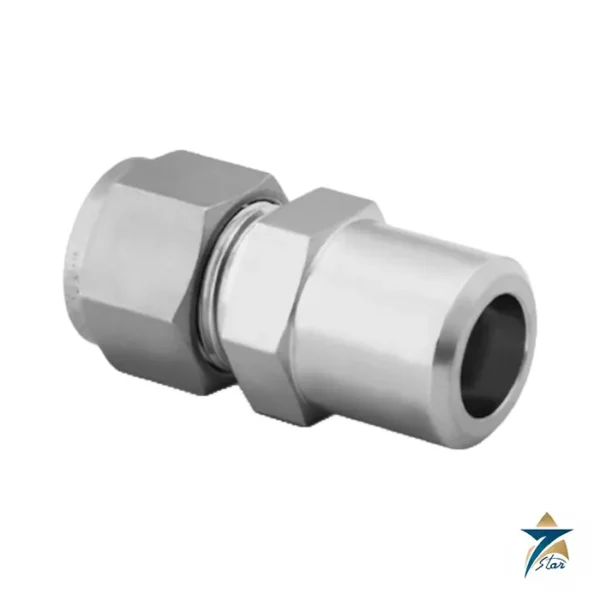
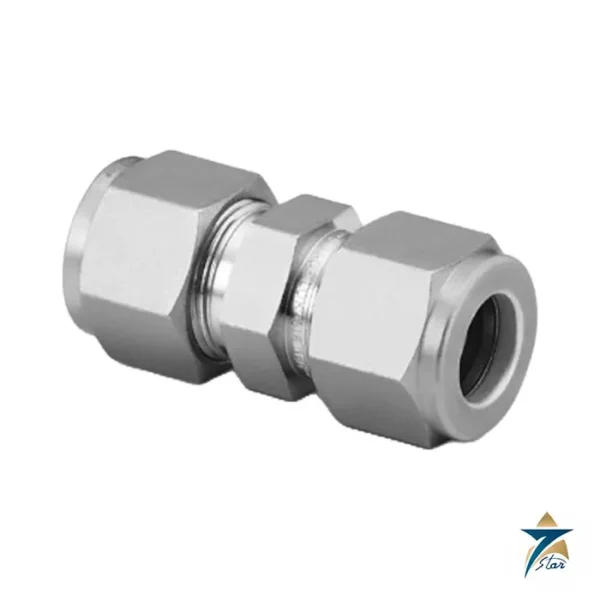
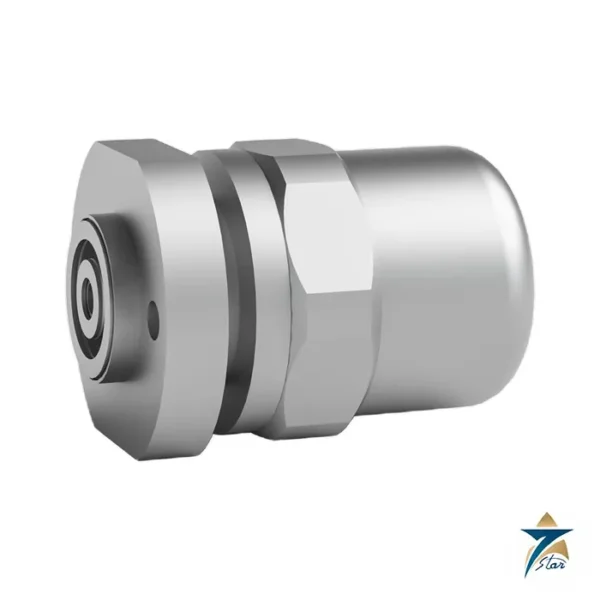
The Swagelok SS-810-6-8W joins a 1/2 in. tube-fitting connection to a welded tube. One end is the standard Swagelok port with nut and ferrules; the other is a socket that takes the end of a 1/2 in. tube, which is then fillet-welded in place. It is the usual way to take a hard-piped tube run to a demountable instrument connection without a pipe thread.
Technical specifications
| Parameter |
Specification |
| Part number |
SS-810-6-8W |
| Description |
Tube socket weld union, 1/2 in. tube fitting x 1/2 in. tube socket |
| Body material |
316 stainless steel |
| Tube-fitting end |
1/2 in. tube OD |
| Socket weld size |
1/2 in. |
| Dimension A (overall length) |
1.62 in. |
| Dimension B (socket depth) |
0.38 in. |
| Dimension D (nut size) |
0.90 in. |
| Dimension E (nominal opening) |
0.41 in. |
| Dimension J (weld end diameter) |
0.73 in. |
| Cleaning |
Standard cleaning and packaging SC-10 |
Socket weld geometry
In the catalog table for tube socket weld fittings, the 1/2 in. entry shows overall length A of 1.62 in., socket depth B of 0.38 in. and weld-end diameter J of 0.73 in. The tube bottoms against the socket shoulder and is seal-welded around the outside, leaving the tube-fitting end free for a normal Swagelok connection. The nominal opening E is 0.41 in., equal to the bore of the 1/2 in. union SS-810-6, so the weld version does not narrow the flow path.
A is 1.62 in., shorter than the 2.02 in. of the ordinary union, because the socket end replaces the second nut and ferrule set.
Choosing between socket and pipe weld
A socket weld union takes tube; the male pipe weld connector SS-810-1-8W takes a pipe stub. Use the socket type when the process line is tube (for example 1/2 in. OD stainless tube in an instrument loop) and pipe weld when the line is NPS pipe. In both cases the W in the number identifies the weld end and 8 refers to the 1/2 in. weld size.
SS-810-6-8W decodes as 316 stainless, 1/2 in. tube, union body, 1/2 in. socket, weld. Sizes from 1/8 in. to 1 in. are listed in the catalog, for example SS-400-6-4W for 1/4 in. and SS-1210-6-12W for 3/4 in.
Welding and fit-up notes
Follow your qualified welding procedure. Keep the Swagelok nut and ferrules off the body during welding to avoid heat damage, or weld first and fit the tube-fitting hardware afterwards. Let the weld cool, clean the joint and inspect it to the standard your project calls for. Then complete the tube-fitting end with one and one-quarter turns of the nut from finger-tight, confirming pull-up with the gap inspection gauge.
The weld joint rating comes from the welded tube and procedure rather than from the fitting body; the Swagelok end is rated to the tubing fitted. Document the weld and tube data so the system limit can be traced.
Selection checks before ordering the SS-810-6-8W
Confirm three things before this union goes on the bill of materials. First, check that the line really is 1/2 in. OD tube on both sides: a metric tube or an NPS pipe of similar appearance will not fit correctly, and mixing tube standards in one system is a common source of leaks. Second, compare the tube wall thickness and material with the duty, since the pressure rating of the finished joint depends on the tubing and the weld, not on the union body alone. Third, make sure the welding procedure and welder qualification required by the project cover socket welds in stainless steel of this size. Where the system carries a corrosive process fluid, ask the process or materials engineer to confirm that 316 stainless steel is acceptable for both the fitting and the tube.
Preparing the tube and making the joint
Cut the tube square with a proper tube cutter or saw and deburr the inside and outside edges, so the end seats cleanly against the socket shoulder and no burrs are left in the bore. Clean the tube end and the socket of oil, marker ink and dirt before fit-up. Socket welding practice in many codes calls for a small axial gap between the tube end and the bottom of the socket to allow for weld shrinkage; follow the gap and fit-up rule in your welding procedure rather than pushing the tube hard against the shoulder if the procedure says otherwise. Use a purge on the inside where the procedure requires it, which helps protect the inner surface of stainless steel from heat discolouration.
Testing and handover
After welding and inspection, assemble the tube-fitting end and pressure test the line according to the project test procedure, using the medium and test pressure the system design specifies. Check the tube-fitting end with the gap inspection gauge once more after testing, and tag the joint or record it on the isometric drawing with the weld number. Keep the inspection records with the material certificates so the line can be traced during later audits.
Maintenance and disconnection
The tube-fitting end of the union is the part intended to be opened. When reconnecting after disconnection, follow the Swagelok reassembly instructions in the catalog rather than repeating the initial turn count. Inspect the connection for leaks after reassembly and during routine walk-downs.
Installation conditions in Oman and the GCC
Instrument tubing on Gulf plants is often outdoors, exposed to strong sun, wide daily temperature swings and, at coastal sites, salt-laden air. Support tube runs properly so thermal expansion does not load the welded joint or the tube-fitting end, and keep runs away from surfaces where wind-blown sand and salt collect. During welding outdoors, protect the work area from wind and dust, which can disturb shielding gas and contaminate the joint, and clean the finished weld area before inspection.
Documents and quotation
The Swagelok catalog MS-01-140 is the source for the tables and rules on this page and is attached for download. For a quotation please give us the full part number SS-810-6-8W, the quantity and any packaging requirement. The catalog table for tube socket weld fittings gives the dimensions summarised here.
Related items: product category.




Reviews
There are no reviews yet.