
- Vibration Monitoring
- Industrial Communications
- PLC & I/O Cards
- Automation Accessories
- Controllers & Data Acquisition
- AC Drives
- Industrial Computers
- Encoders
- Safety Switches & Guard Locking
- Isolator & Barrier
- Automation Software
- HMI Displays
- Motor Soft Starters
- Servo Drives
- CCTV & Security
- Robotics
- Pneumatic Cylinders
- Machine Vision
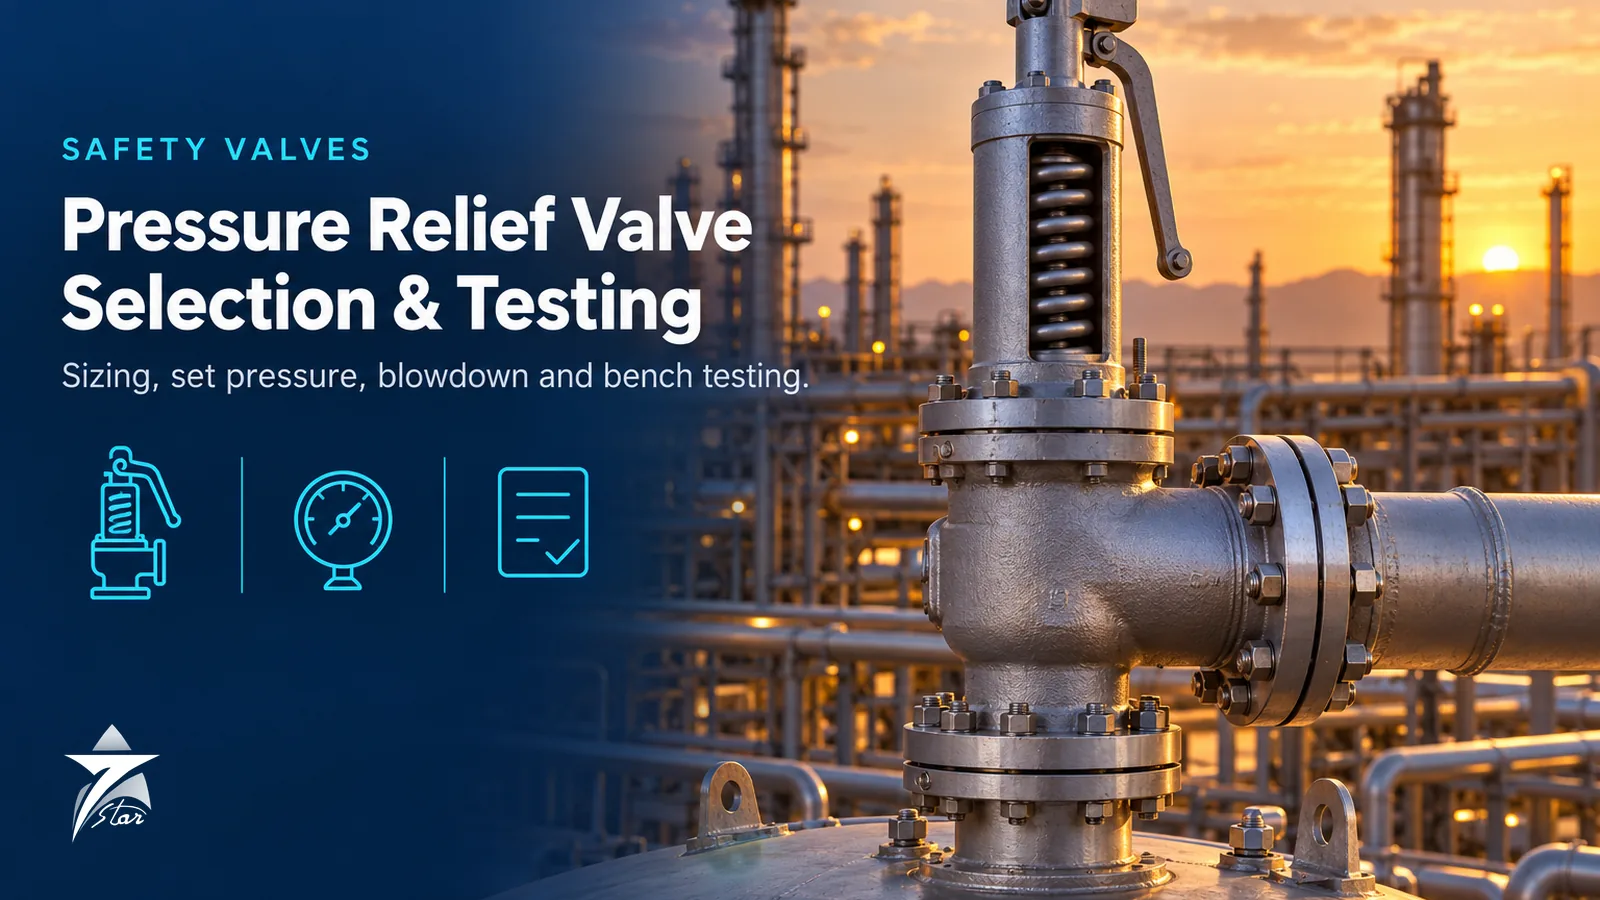
Pressure Relief Valve Guide: Types, API 520/526 Sizing Basics, Set Pressure, Testing and Maintenance
A pressure relief valve is the last mechanical layer of protection between a process upset and a ruptured vessel. It works only if the set pressure is right, the valve was sized for the governing scenario, the inlet and outlet piping let it open and close cleanly, and someone tested it on schedule. Otherwise it may chatter, fail to lift, or leak until operations isolate it and leave the equipment unprotected.
This guide covers terminology, valve types, API 520 and API 526 sizing basics, installation rules and testing practice for engineers maintaining relief valves on oil and gas, refining, power and desalination plants in Oman and the GCC.
Terminology the Codes Depend On
In API and ASME usage, a safety valve opens rapidly to full lift (pop action) and is used on steam, gas and vapour. A relief valve opens progressively in proportion to overpressure and is used mainly on liquids. A safety relief valve can work in either mode depending on the fluid. “Pressure relief valve” is the umbrella term used throughout API 520.
| Term | Meaning | Typical value or source |
|---|---|---|
| Set pressure | Inlet gauge pressure at which the valve is adjusted to open under service conditions | ASME VIII tolerance typically ±2 psi (±0.14 bar) up to 70 psi, ±3% above |
| MAWP | Maximum allowable working pressure of the protected equipment at coincident temperature | Vessel nameplate; at least one valve set at or below MAWP |
| Overpressure | Pressure rise above set pressure during discharge, % of set pressure | Equals accumulation when set pressure equals MAWP |
| Accumulation | Pressure rise above MAWP during discharge, % of MAWP | ASME VIII: 10% single valve, 16% multiple valves, 21% fire case |
| Blowdown | Difference between set pressure and reseating pressure, % of set | Typically 7–10% on many process valves; confirm on the datasheet |
| Superimposed backpressure | Pressure at the outlet before the valve opens, constant or variable | Flare or vent header study |
| Built-up backpressure | Pressure at the outlet caused by flow through the valve | Outlet line hydraulic calculation |
| CDTP | Cold differential test pressure: bench set pressure corrected for backpressure and temperature | Stamped on the nameplate |
Under ASME Section VIII Division 1, the 10% and 16% accumulation limits apply with a minimum of 3 psi and 4 psi respectively. In multiple-valve installations, one valve must be set at or below MAWP and additional valves may be set up to 105% of MAWP. For the fire case, supplemental valves may be set up to 110% of MAWP.
How the Main Valve Types Work
Conventional spring-loaded valves
The bonnet is vented to the outlet, so backpressure adds to the spring force: variable superimposed backpressure shifts the opening point and built-up backpressure reduces lift and capacity. As a general guide, built-up backpressure on a conventional valve is limited to about 10% of set pressure when 10% overpressure is allowed.
Balanced bellows valves
A bellows with an effective area equal to the seat area isolates the top of the disc from backpressure. The set pressure becomes largely independent of backpressure, and the valve tolerates much higher built-up backpressure, with a capacity correction factor (Kb) taken from the manufacturer’s curves. The bonnet vent must stay open: a plugged or painted-over vent destroys the balance. If the bellows ruptures, process fluid escapes through the vent, so for toxic or flammable fluids the vent must be piped to a safe location.
Pilot-operated valves
Process pressure acts on a dome above a piston whose area is larger than the seat area, so rising pressure seals tighter. A small pilot senses inlet pressure and vents the dome at set pressure, either with pop action or modulating so the main valve opens only as far as needed. Pilot valves stay tight close to set pressure and can use remote sensing to remove inlet-loss effects. Their weakness is small sensing passages, which plug in dirty, waxy or hydrate-forming service unless filters or purge are fitted.
| Feature | Conventional | Balanced bellows | Pilot-operated |
|---|---|---|---|
| Backpressure tolerance | Low; built-up typically ≤10% of set | High; follow Kb curves | High with backflow preventer |
| Normal operating pressure vs set | Typically up to about 90% | Typically up to about 90% | Often 95% or higher |
| Dirty, viscous or solids-laden service | Good | Good; bellows protects spring | Poor without filters or purge |
| Seat tightness near set pressure | Simmer and leakage possible | Simmer and leakage possible | Very good |
| Typical use | Clean utilities, atmospheric discharge | Flare headers with variable backpressure | Large orifices, high backpressure, tight margins |
Relief Scenarios and Sizing Basics
API 521 defines the overpressure scenarios. Common ones are blocked outlet, external fire, tube rupture, control valve failure including gas blow-by, blocked-in liquid thermal expansion and utility failure. For tube rupture, API 521 allows the scenario to be excluded when the low-pressure side is protected by the 10/13 rule. The governing case is the scenario that requires the largest relieving area, not the sum of all scenarios.
API 520 Part I gives the sizing equations for gas and vapour at critical and subcritical flow, steam, liquid, and two-phase flow (the omega method in its annex). Relieving pressure is set pressure plus allowable overpressure plus atmospheric pressure. Correction factors include Kb for backpressure on bellows valves, Kc = 0.9 for a rupture disc upstream of the valve without a certified combination factor, Kw for liquid backpressure on bellows valves, and Kv for viscosity.
For the fire case, API 521 estimates heat input as Q = 21,000·F·A^0.82 (Btu/h, A in ft²) where adequate drainage and prompt firefighting exist, and Q = 34,500·F·A^0.82 where they do not. The wetted area is counted up to 7.6 m (25 ft) above the surface that could sustain a pool fire.
Preliminary sizing uses the API 526 effective areas with effective discharge coefficients (Kd of 0.975 for gas and vapour, 0.65 for liquid). The final check must use the manufacturer’s actual orifice area and certified coefficient. Mixing effective area with certified coefficient, or the reverse, is a classic error that can undersize a valve.
| API 526 orifice | Effective area (in²) | Effective area (mm²) | Common inlet x outlet designations |
|---|---|---|---|
| D | 0.110 | 71 | 1D2, 1.5D2 |
| E | 0.196 | 126 | 1E2, 1.5E2 |
| F | 0.307 | 198 | 1.5F2, 1.5F3 |
| G | 0.503 | 325 | 1.5G3, 2G3 |
| H | 0.785 | 506 | 1.5H3, 2H3 |
| J | 1.287 | 830 | 2J3, 3J4 |
| K | 1.838 | 1,186 | 3K4, 3K6 |
| L | 2.853 | 1,841 | 3L4, 4L6 |
| M | 3.60 | 2,323 | 4M6 |
| N | 4.34 | 2,800 | 4N6 |
| P | 6.38 | 4,116 | 4P6 |
| Q | 11.05 | 7,129 | 6Q8 |
| R | 16.0 | 10,323 | 6R8, 6R10 |
| T | 26.0 | 16,774 | 8T10 |
API 526 also standardises flange ratings and centre-to-face dimensions for flanged steel valves, making valves broadly interchangeable on the same letter and size. Confirm dimensions on the datasheet before replacing a valve in existing pipework. In Europe, EN ISO 4126 applies, so check which code the vessel was designed to.
Installation: API 520 Part II
- Keep non-recoverable inlet pressure loss at or below 3% of set pressure at rated capacity. Recent editions allow an engineering analysis where this cannot be met, but 3% remains the default design target. Short, large-bore inlets with rounded entrances help; remote-sensed pilots are another route.
- Keep built-up backpressure within the limit of the valve type.
- Isolation valves upstream or downstream must be full bore and car-sealed or locked open under an administrative procedure.
- Mount valves upright, avoid liquid pockets at the inlet, and drain the low point of atmospheric discharge lines so rainwater cannot collect on the disc.
- Where a change-over valve arrangement is used to allow one valve to be removed with the plant running, include its pressure loss in the 3% inlet budget and make sure the mechanism always leaves one full flow path open.
Why Relief Valves Chatter
Chatter hammers the seat and guides, fatigues bellows and can cut capacity well below rated. Usual causes:
- Oversizing, where the actual relief flow is a small fraction of rated capacity (often quoted as below about 25–30%), so the valve cannot stay open.
- Inlet pressure loss above 3% of set pressure, so pressure at the valve collapses when it opens.
- Excessive built-up backpressure on a conventional valve.
- Pressure-wave interaction in long inlet lines.
- Operating pressure too close to set pressure, causing simmer.
Remedies include staggered smaller valves, modulating pilots, restricted-lift designs where permitted, and corrected piping.
Testing, Inspection and Recertification
Workshop practice starts with an as-received pop test before disassembly; it shows whether the valve would have protected the equipment and is the key input to risk-based inspection. The valve is then dismantled, inspected, lapped and set to its CDTP. Seat tightness is checked to API 527, typically at 90% of set pressure for valves set above about 50 psig (3.4 barg).
In-situ lift-assist testing verifies set pressure without removal but does not prove seat tightness or capacity.
Intervals come from the inspection code and the plant’s risk-based inspection program. API 510 commonly cites maximum intervals of five years for typical process service and up to ten years for clean, non-fouling services, while API 576 gives inspection and repair guidance for the devices themselves. Fouling, corrosive or polymerising service and any history of failed as-received tests justify shorter intervals. Test benches and reference gauges must themselves be calibrated; see our instrument calibration program guide.
Oman Site Considerations
- Sour service: wetted parts, including springs exposed to the fluid in conventional designs, must meet NACE MR0175/ISO 15156 where H2S is present. A bellows can isolate the spring from the process.
- Sand and produced solids: nozzle and disc erosion after each lift causes seat leakage; inspect seats after any relieving event.
- Heat: 45–50 °C ambient plus solar gain pushes soft seats and pilot O-rings toward their limits; check elastomer ratings against metal temperature.
- Coastal salt at Sohar, Duqm, Sur and Salalah: external corrosion of bolting, levers and open-bonnet springs; specify coatings and weather hoods.
- Remote unmanned stations: holding a pre-tested spare for each critical tag allows swap-and-test without extending outages.
The relief valve sits below the instrumented layers in the protection hierarchy; our article on safety instrumented systems explains how SIS and mechanical relief complement each other.
Common Mistakes
- Sizing on the API 526 effective area and then ordering on the manufacturer’s actual area without rechecking the coefficient.
- Selecting a conventional valve for a flare header with variable superimposed backpressure.
- Plugging or painting over the bellows bonnet vent.
- Using a pilot valve on waxy crude or hydrate-forming gas without filters.
- Setting the valve at ambient conditions without the CDTP correction for temperature and backpressure.
Selection and Procurement Checklist
- Governing relief scenario and required relieving rate, with the API 521 basis documented.
- Fluid, phase, molecular weight, density, viscosity, Z and k at relieving conditions.
- Set pressure, MAWP, allowable overpressure and CDTP.
- Superimposed (constant and variable) and built-up backpressure.
- Valve type: conventional, balanced bellows or pilot-operated, with justification.
- API 526 orifice letter and inlet x outlet size, flange ratings and facing.
- Body, trim, spring and soft goods materials, including NACE MR0175/ISO 15156 where sour.
- Seat tightness requirement (API 527 or stricter), lifting lever and cap type.
- Change-over valve or isolation arrangement, with car-seal procedure.
- Code stamp and certification required (ASME, EN ISO 4126, PED as applicable).
Sourcing Pressure Relief Valves Through Seven Star LLC
Seven Star LLC supplies and sources relief valves and spares across the main design families. For API-dimensioned flanged process valves, see the LESER Type 526. Demanding duties are covered by the LESER Critical Service series and the LESER High Pressure series, while compact designs are in the LESER Compact Performance series. Where a proportional opening characteristic is wanted, review the LESER Modulate Action series against your service conditions. For maintenance without shutdown, see the LESER change-over valve series and the LESER Type 310. Pilot-operated options include the Anderson Greenwood Series 90/9000. The full range is in our safety relief valves category and on the LESER brand page.
Send your relief valve datasheets or nameplate photos to Seven Star LLC and our team will source the matching valves, spares or change-over assemblies for your plant.
Was this guide helpful?One click helps us write better guides for engineers.
Thank you! Glad it helped. Need this equipment for your project? Request a quotation
Thank you. We will use this to improve the guide.
Need a Quotation for Your Project?
Seven Star LLC supplies the industrial equipment covered in this article to customers across Oman and the GCC. Send us the part numbers, models or a short description with quantities, and our sales team will reply with a formal quotation.
- Genuine OEM products
- Supply across Oman & the GCC
- Formal quotation from our sales team
Free, no-obligation quotation · takes about 1 minute
Other enquiries: [email protected] · WhatsApp
More Blog


Frequently Asked Questions
A safety valve opens rapidly to full lift at set pressure and is used for steam, gas and vapour. A relief valve opens progressively as pressure rises above set and is used mainly for liquids. A safety relief valve is designed to work in either mode, and pressure relief valve is the general term covering all three.
Under ASME Section VIII Division 1, accumulation above MAWP is limited to 10% for a single valve, 16% for multiple valves and 21% for the external fire case, with small minimum values at low pressures. When the set pressure equals MAWP, allowable overpressure equals these accumulation limits. Other codes such as EN ISO 4126 and pressure equipment regulations have their own rules.
The most common causes are an oversized valve relieving only a small fraction of its rated capacity, inlet pressure loss above 3% of set pressure, and excessive built-up backpressure on a conventional valve. Chatter damages the seat and guides and can reduce capacity. Staggered smaller valves, modulating pilots or corrected inlet piping usually solve it.
Intervals are set by the inspection code and the plant's risk-based inspection program. API 510 commonly cites up to five years for typical process service and up to ten years for clean, non-fouling service, with shorter intervals for fouling or corrosive duty. A failed as-received test should shorten the interval for that valve.
Use a balanced bellows valve when superimposed backpressure varies, as in a shared flare header, or when built-up backpressure exceeds what a conventional valve tolerates. The bellows also protects the spring and guide from corrosive or fouling fluid. The bonnet vent must remain open and be routed to a safe location for hazardous fluids.
Only with precautions, because the pilot's small sensing passages can plug with solids, wax, hydrates or polymer. Manufacturers offer filters, purge arrangements and remote sensing for such duties. For heavily fouling service, a conventional or bellows spring-loaded valve is usually the safer choice.