Rutile fast-freezing duplex wire for positional work
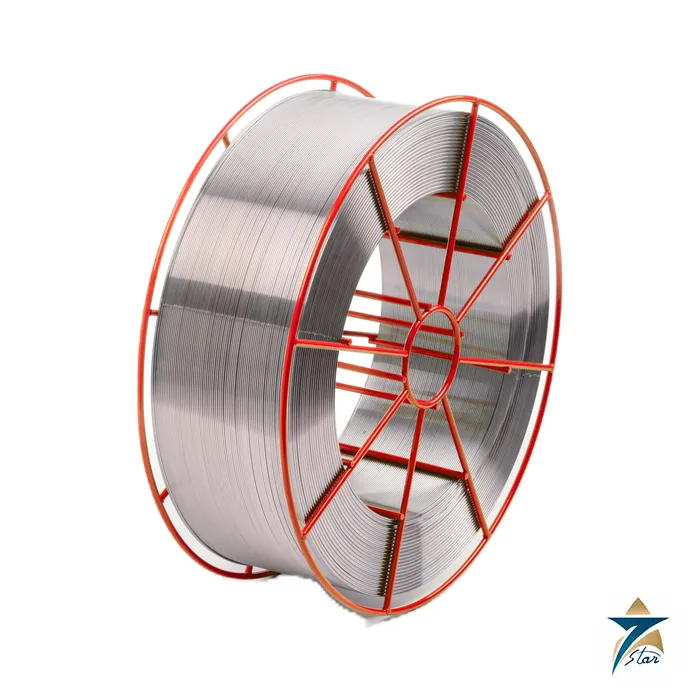
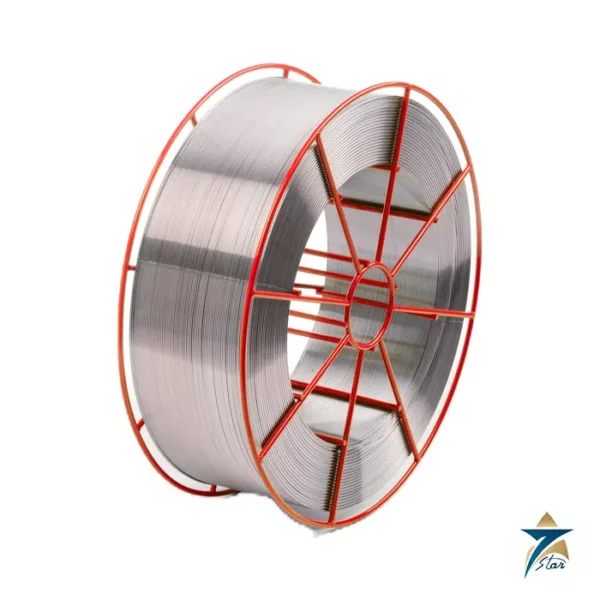
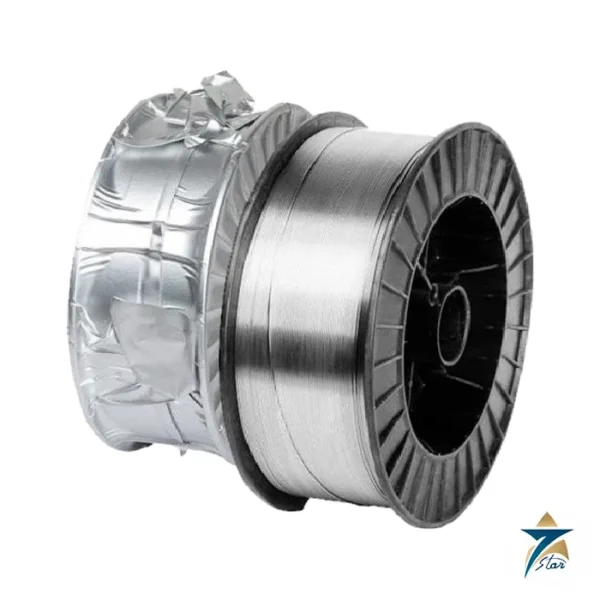
The Selectarc FCW 2209P is a gas-shielded flux-cored wire for all-position welding of duplex stainless steels such as 2205 and 2304. It is classified AWS A5.22 E2209T1-1/-4 and ISO 17633-A T 22 9 3 N L P M21 (C1) 1. A rutile, fast-freezing slag supports the weld pool in vertical and overhead positions, which makes the wire suited to pipe spools, structural nodes and vessel nozzles that cannot be turned.
Selectarc states resistance to severe corrosive environments, including intergranular attack, pitting, crevice and stress corrosion, and a PREN above 35. Main applications are pumps, vessels and piping attacked by chloride-containing solutions, as well as impellers and other parts that need high strength together with corrosion resistance.
Technical specifications
| Parameter |
Specification |
| Manufacturer / product |
Selectarc / FCW 2209P |
| Process |
FCAW, gas shielded |
| AWS classification |
A5.22 E2209T1-1/-4 |
| ISO classification |
17633-A T 22 9 3 N L P M21 (C1) 1 |
| Slag type |
Rutile, fast freezing, all positions |
| Weld metal composition, min–max % |
C max 0.04, Si max 1.0, Mn 0.5–2.0, Cr 21.0–24.0, Ni 7.5–10.0, Mo 2.5–4.0, Cu max 0.5, N 0.08–0.20, P max 0.030, S max 0.025 |
| Typical composition, % |
C 0.03, Si 0.80, Mn 1.1, Cr 23.0, Ni 9.0, Mo 3.1, N 0.15 |
| PREN |
Above 35 |
| Rp0.2 (min / typical) |
450 / 630 MPa |
| Rm (min / typical) |
690 / 780 MPa |
| Elongation A5 (min / typical) |
20 / 28% |
| Impact energy KV (typical) |
35 J at -60 °C |
| Diameter and parameters |
1.2 mm: 130–270 A, 22–35 V, stick-out 12–25 mm |
| Current type |
DC, electrode positive |
| Shielding gas |
ISO 14175 M21 (Ar/CO2), 10–20 l/min |
Base metals and fit with other processes
Base materials listed are UNS S31803 (X2CrNiMoN22-5-3, 1.4462), S32304 (X2CrNi23-4, 1.4362) and S32900 (329, 1.4460). Flux-cored duplex wire is often used for fill and cap passes after a GTAW root, delivering much higher deposition than stick electrodes while still allowing positional welding on fixed joints.
The -1/-4 suffix shows that the wire is classified with both CO2 and argon/CO2 mixtures, although Selectarc gives M21 as the recommended gas. For super duplex parent metals, the 25 9 4 type FCW 2509MOP is the matching Selectarc option.
Welding guidance
Run the 1.2 mm wire on DC positive between 130 and 270 A and 22 to 35 V, with a stick-out of 12 to 25 mm and a gas flow of 10 to 20 l/min. Use the lower end of the range for vertical-up and overhead passes, where the fast-freezing slag does most of the work, and higher settings for flat fill passes.
Duplex phase balance depends on heat input and interpass temperature, so set limits in the WPS and verify them with ferrite measurements during qualification. Remove all slag between passes, protect the wire from moisture, and keep wind away from the arc on site, since loss of shielding causes porosity and nitrogen loss in the deposit.
Rutile flux-cored deposits contain more oxygen than GTAW weld metal, which slightly reduces impact energy at very low temperatures. If the design calls for toughness well below -60 °C, check the typical values above against the specification before selecting the process.
Documents and quotation
Download the Selectarc FCW 2209P data sheet attached to this page. More wires are listed in our Flux-Cored Wire category.
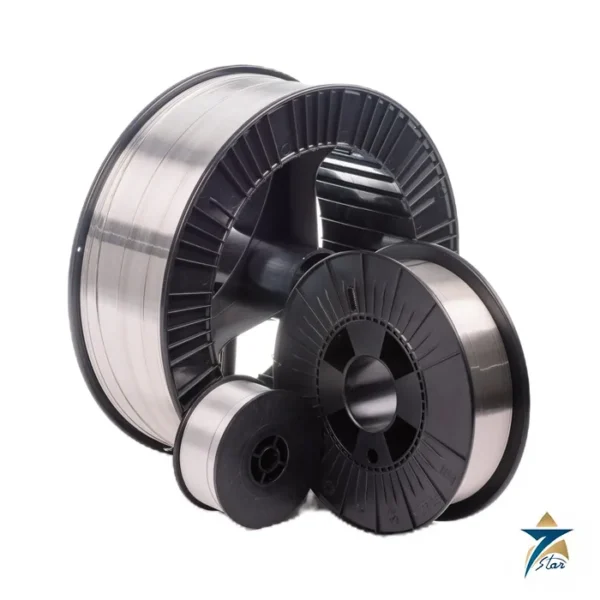
For a quotation, send spool type, quantity and certificate requirements.

Reviews
There are no reviews yet.