
Lincoln Electric Lincolnweld L-61 EM12K Submerged Arc Welding Wire
Overview
Lincoln Electric Lincolnweld L-61 is a mild steel solid electrode for submerged arc welding (SAW), classified AWS EM12K. Lincoln Electric describes it as the industry standard for submerged arc applications: a low carbon, medium manganese, low silicon general purpose wire that suits a wide range of single pass and multiple pass work. In pressure vessel shops, pipe mills, tank fabrication yards and structural beam lines, an EM12K wire paired with a suitable flux is one of the most common ways to deposit heavy welds quickly and with consistent quality.
Seven Star LLC supplies Lincoln Electric Lincolnweld L-61 to fabricators and EPC contractors in the Sultanate of Oman and the GCC. Our Muscat team can provide the manufacturer datasheet, advise on wire diameter and package, and help you pair the wire with an appropriate Lincolnweld flux for your steel and joint design.
How the Submerged Arc Process Uses This Wire
In submerged arc welding a bare wire is fed into a blanket of granular flux. The arc burns beneath the flux, so there is no visible arc flash and almost no spatter, and the flux melts to form a slag that protects and shapes the weld. Because current densities are very high and the flux traps heat, deposition rates are several times those of stick or gas metal arc welding on thick material. The wire is therefore chosen for its chemistry and its interaction with the flux, and it is normally qualified together with that flux for a specific classification.
The EM12K class that applies to Lincoln Electric Lincolnweld L-61 is a medium manganese wire with silicon added. The K in the designation shows that the wire is silicon killed, meaning that it contains deoxidisers that help the weld metal stay clean. The datasheet for Lincoln Electric Lincolnweld L-61 prints the composition limits as carbon 0.05 to 0.15 percent, manganese 0.80 to 1.25 percent, silicon 0.10 to 0.35 percent, sulphur 0.030 percent maximum, phosphorus 0.030 percent maximum and copper 0.35 percent maximum, and notes that single values are maximums.
Engineering Design and Packaging of Lincoln Electric Lincolnweld L-61
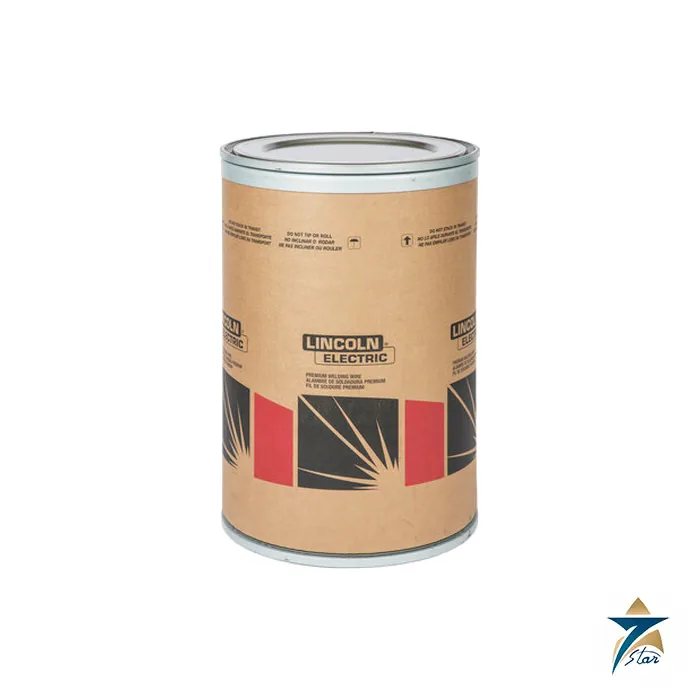
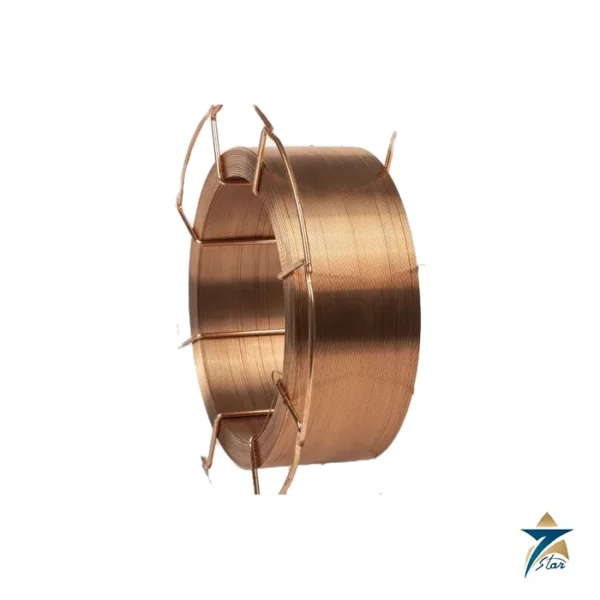
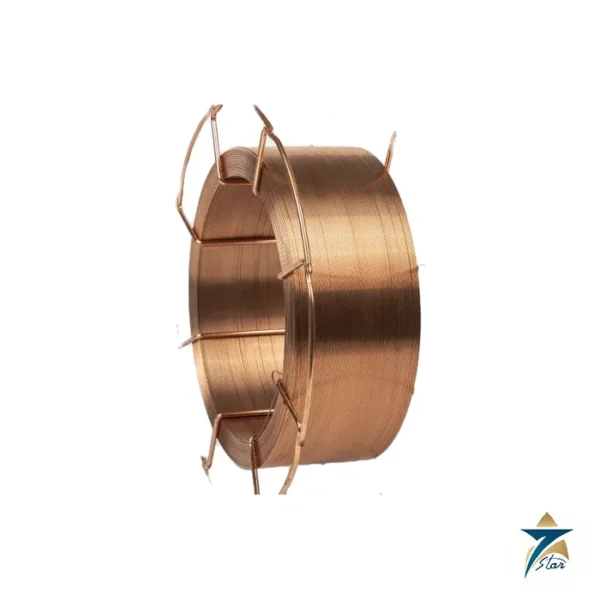
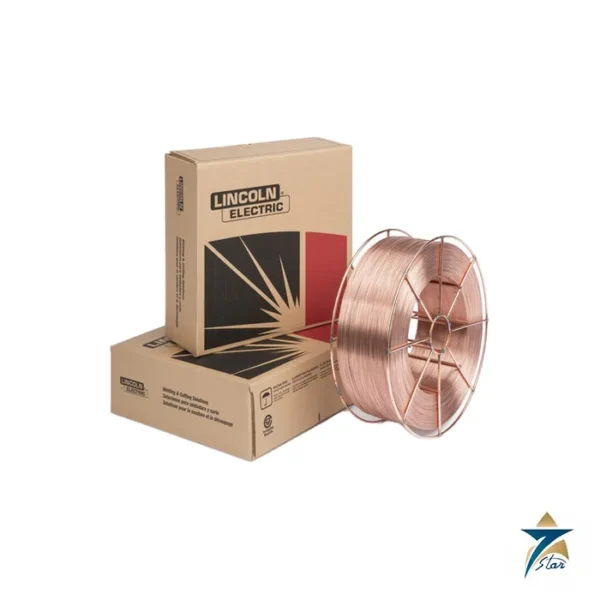
Lincoln Electric Lincolnweld L-61 is a solid submerged arc wire supplied in coils, reels and drums. Lincoln Electric lists diameters of 1/16 inch (1.6 mm), 5/64 inch (2.0 mm), 3/32 inch (2.4 mm), 1/8 inch (3.2 mm), 5/32 inch (4.0 mm) and 3/16 inch (4.8 mm). Reference packages in the datasheet include 60 lb coils, 250 lb Speed Feed SlimReel packages, 300 lb Speed Feed reels and drums, 600 lb and 1000 lb Speed Feed drums, a 750 lb Speed Feed reel and a 2200 lb Speed Feed stem. Not every diameter is offered in every package. These are the manufacturer reference packages, not a statement of Seven Star stock, so request current availability.
For traceability, the manufacturer states that actual Type 3.1 certificates showing the chemical composition of each lot of Lincoln Electric Lincolnweld L-61 are available in its certificate centre. Buyers working to client inspection plans should request the lot certificate with the order.
Key Features of Lincoln Electric Lincolnweld L-61
The following points come from the manufacturer datasheet:
- A low carbon, medium manganese, low silicon general purpose submerged arc electrode.
- Industry standard status for submerged arc welding, with a long record on structural and pressure equipment.
- A good choice for a wide range of applications with single or multiple pass welds.
- Conformance to AWS A5.17/A5.17M EM12K and AWS A5.23 EM12K, as well as MIL-E-23765/4 MIL-EM12K and EN 756 S2Si.
- Recommended for use with a broad list of Lincolnweld fluxes, so the flux can be selected to suit the joint and the steel.
- Actual Type 3.1 certificates for each lot, showing chemical composition, available from the manufacturer.
- A wide range of diameters from 1/16 to 3/16 inch and package options from coils to 2200 lb stems.
Recommended Fluxes
The datasheet lists the following Lincolnweld fluxes as recommended companions for Lincoln Electric Lincolnweld L-61: 760, 761, 780, 781, 860, 865, 882, 888, 761-Pipe, P223, 960, 980, WTX, AXXX-10, 995N and SPX80. Active fluxes such as the 700 series add manganese and silicon and are often chosen for single pass or limited pass welds on clean plate, while neutral fluxes such as the 800 and 900 series keep the deposit chemistry closer to the wire and are the usual choice for multiple pass welds and thicker joints. This is general class information; confirm the correct pairing against the manufacturer flux datasheet and your procedure qualification.
Industrial Applications in Oman and the GCC
Submerged arc wire like Lincoln Electric Lincolnweld L-61 is used wherever long, heavy welds are made in a shop: longitudinal and circumferential seams on pressure vessels and storage tanks, structural beams and girders, spiral and straight seam pipe, and pipe spools prepared for oil and gas and water projects. Oman’s fabrication clusters at Sohar, Rusayl and Duqm, plus the water transmission and desalination programmes around the Gulf, provide consistent demand for such heavy shop welds, where a continuous automatic process saves labour and increases repeatability.
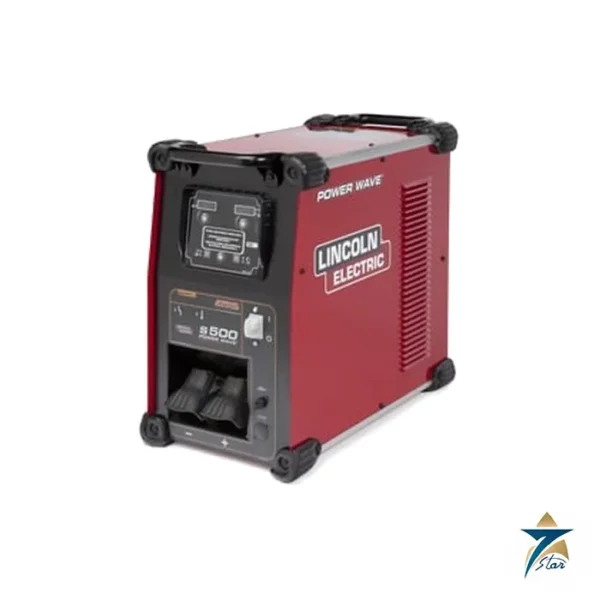
Seven Star LLC supplies Lincoln Electric Lincolnweld L-61 together with welding equipment for the rest of the fabrication line. For flux-cored and gas-shielded processes, buyers often review the Lincoln Electric Power Wave S500 and the ESAB Rebel EMP 285ic, and our team also lists items such as the Kobelco Lubricator Assembly for plant owners.
Technical Specifications of Lincoln Electric Lincolnweld L-61
The table lists values printed in the Lincoln Electric Lincolnweld L-61 datasheet. The datasheet does not print typical mechanical properties for this wire, because the properties depend on the flux used; ask the supplier for the test certificate for your flux and wire lot.
| Parameter | Specification |
|---|---|
| Model | Lincoln Electric Lincolnweld L-61 |
| Electrode type | Mild steel solid submerged arc (SAW) electrode |
| AWS classification | AWS A5.17/A5.17M EM12K; AWS A5.23 EM12K |
| Other conformances listed | MIL-E-23765/4 MIL-EM12K; EN 756 S2Si |
| Wire composition | C 0.05-0.15; Mn 0.80-1.25; Si 0.10-0.35; S 0.030 max; P 0.030 max; Cu 0.35 max (percent; single values are maximums) |
| Diameters | 1/16, 5/64, 3/32, 1/8, 5/32, 3/16 in (1.6, 2.0, 2.4, 3.2, 4.0, 4.8 mm) |
| Reference packages | 60 lb coil; 250 lb Speed Feed SlimReel; 300 lb Speed Feed reel and drum; 600 lb and 1000 lb Speed Feed drum; 750 lb Speed Feed reel; 2200 lb Speed Feed stem |
| Recommended fluxes | Lincolnweld 760, 761, 780, 781, 860, 865, 882, 888, 761-Pipe, P223, 960, 980, WTX, AXXX-10, 995N, SPX80 |
| Certificates | Type 3.1 lot certificates available from the manufacturer |
Handling, Storage and Flux Practice
Keep Lincoln Electric Lincolnweld L-61 in its original packaging until it goes into the feeder, store it in a dry area and cover opened reels and drums. Rust or oil on the wire surface increases hydrogen and porosity risk. Fluxes are hygroscopic and should be kept dry and re-dried according to the flux manufacturer instructions before use if they have taken on moisture. This is general welding guidance, not a Lincoln Electric warranty statement.
Call To Action
To order Lincoln Electric Lincolnweld L-61, send Seven Star LLC your diameter, package type, quantity and the flux you plan to use, and our Muscat team will prepare a formal quotation and confirm availability for delivery across Oman and the GCC. The manufacturer datasheet is attached to this page. Seven Star LLC supplies Lincoln Electric as a trusted supplier with engineering support in Muscat, so contact us with your enquiry and we will help with documentation and delivery.
- Datasheet Lincoln Electric Lincolnweld L-61 datasheet (manufacturer publication) Download
Browse Lincoln Electric products by category: Welding Equipment.


Reviews
There are no reviews yet.